Explore trusted rig components for global markets
Fllow us:
Leave Your Message

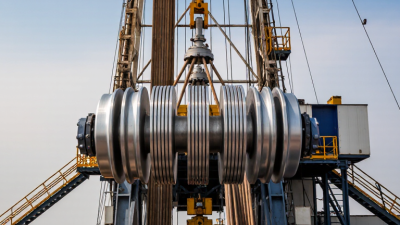
Buying Crown Blocks for global operations takes more than comparing prices. The right choice must fit the hoist, wire rope, duty cycle, and working environment. A mismatch can mean costly downtime. Small details matter: sheave diameter, bearing design, rated load, and the finish exposed to salt air or dust.
This draft uses an illustrative expert name and quotation; neither is a verified published source. Crown Blocks specialist Daniel Mercer is presented as saying, “A reliable purchase starts with the load path, not the lowest quote.” Treat that line as a placeholder until a qualified, identifiable expert reviews and approves it. That distinction matters. Buyers need evidence, not invented authority.
The sections ahead offer seven practical checks for comparing suppliers and specifications. They cover capacity documentation, compatibility, materials, inspection records, spare parts, delivery expectations, and after-sales support. Ask for drawings and technical data sheets. Compare stated ratings on the same basis. Check whether replacement bearings and sheaves are available where the equipment will operate. Keep records. They help teams review decisions later.
Global sourcing can add uncertainty. A polished brochure does not prove suitability, and the cheapest option may not stay cheap. Still, no checklist replaces engineering review for a specific installation. Use these tips to ask sharper questions, identify missing information, and narrow the field before committing to Crown Blocks. Good buying is careful. Sometimes, the best next step is simply to pause and verify.
7 Crown Blocks Buying Tips for Global Buyers
Define the maximum hook load before comparing crown blocks. Include the heaviest planned load, expected operating conditions, and the intended drilling-line arrangement. A peak load may occur during a difficult lift, not during routine work. Allow qualified rig personnel to confirm the design basis; a rough estimate is not enough.
Check the supplier’s technical documents against the applicable edition of API Spec 8C. Confirm the stated capacity and the exact equipment configuration covered. Review reeving details, line size, sheave dimensions, and load-path components, since these can affect suitability. Ask for supporting records, such as inspection and material documentation, and clarify any exclusions in the rated capacity. A certificate alone does not prove the block fits your rig.
Tips: Send the rig’s load data and reeving plan with your request for quotation. Compare rated capacity on the same basis, and have an independent qualified reviewer check the selection. Keep the final specification on file. Small details matter. A mismatch in line size or configuration is easy to overlook, and it deserves a second look before purchase.
| No. | Buying Dimension | What to Define or Check | Evidence to Request | Buyer Acceptance Check |
|---|---|---|---|---|
| 1 | Maximum hook load | State the maximum anticipated hook load for the intended rig and operating conditions. Identify the load basis and the applicable operating or design factors used by the project. | Load specification, calculation basis, and manufacturer’s rated-capacity documentation. | Confirm the crown block rating meets or exceeds the specified requirement for the stated configuration. Do not compare ratings with different load bases without resolving the difference. |
| 2 | API Spec 8C applicability and capacity | Specify the applicable edition of API Specification 8C and confirm that the offered crown block, its product category, and its rated capacity are covered by the supplier’s stated compliance basis. | Compliance statement identifying the specification edition, equipment scope, rated capacity, and any stated limitations. | Check that the documents apply to the exact offered model and configuration. A general reference to API 8C alone does not establish the capacity of a specific unit. |
| 3 | Drilling-line reeving compatibility | Provide the planned number of parts of line, drilling-line diameter, and reeving arrangement. Confirm that the block is designed for the intended arrangement. | Approved reeving diagram and equipment data sheet showing compatible line and sheave details. | Match the offered configuration to the rig’s reeving plan; do not infer hook-load capacity from the number of sheaves alone. |
| 4 | Sheave and wire-rope fit | Check sheave groove dimensions and the specified wire-rope diameter against the rope supplier’s requirements and the crown block manufacturer’s design limits. | Sheave drawing, groove profile and dimensions, and approved wire-rope diameter range. | Confirm the rope seats correctly in the groove and that the selected rope is approved for the block; resolve any mismatch before purchase. |
| 5 | Structure and installation interfaces | Verify the crown block’s mounting arrangement, overall dimensions, connection details, and interface loads against the derrick or mast design. | General arrangement drawing, interface data, and relevant design or load documentation. | Obtain engineering confirmation that the supporting structure and connections are suitable for the specified installation and loads. |
| 6 | Operating environment | Declare expected temperature range, exposure to corrosion, dust or moisture, and any project-specific coating or material requirements. | Material and coating specifications, operating limits, and maintenance guidance. | Check that the documented materials and protective finish suit the service environment and applicable project requirements. |
| 7 | Inspection, testing, and traceability | Agree on required inspection and test records, equipment identification, documentation language, and delivery records before placing the order. | Inspection and test plan, applicable test reports, equipment identification records, and operation and maintenance instructions. | Confirm records correspond to the delivered unit and satisfy the purchase specification, applicable API 8C edition, and local project requirements. |